


 39 / 68

 ELECTRIC.IE
• The Magazine & Website for the Irish Electrical Industry •
37
www.edlireland.ie sales@edlireland.ieTel: 01-427 1444
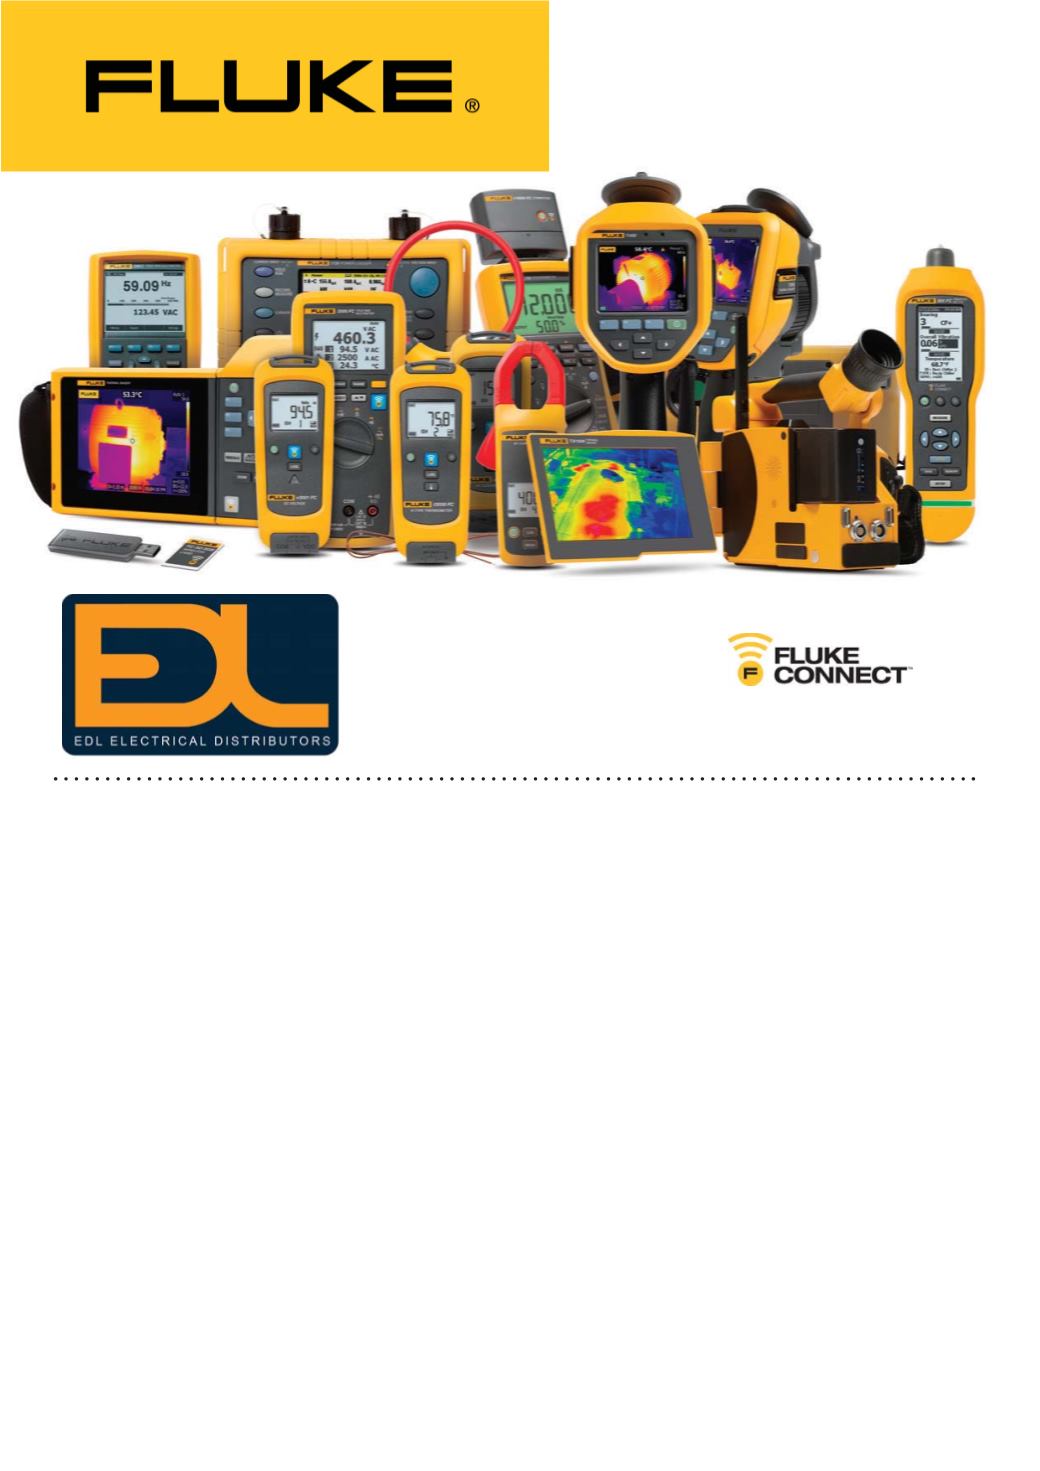
Five reasons to choose a Fluke Infrared Camera from EDL
1. Superior Image Quality:
Fluke maximises the performance
of every pixel throughout their
infrared portfolio with detector
resolution ranging from 1024x768
ͤ͜͢͜ ͜͜͝τ
germanium lenses that give you
crisp detailed images and more
accurate measurements. Get the
image quality you need to pinpoint
the exact location of the problem,
make the right diagnosis and make
the job easier.
2. Pushing the boundaries of
communication with Fluke
Connect:
Save time-wirelessly sync images
directly from your camera to an
asset record or works order using
the Fluke Connect system. Having
access to maintenance records
simultaneously at the inspection
ƥ ơǦ
location enables faster decision
making and real time collaboration
between team members.
3. Premier focus technologies:
Every infrared camera user knows
that if your image is out of focus
temperature measurement could
ơ ͜͞ ǡ
making it easier to miss a problem.
That’s why Fluke engineered
LaserSharp Auto Focus – which uses
a built-in laser distance meter to
instantly calculate and display the
distance to your target so you get an
in-focus image with the touch of a
button.
4. Legendary ruggedness and
ease of use:
Fluke test their cameras to exceed
Ƥ ǡ ǡ
soak them, shock them and shake
them for hours on end. Our tools are
relentless, built tough to withstand
the harsh environments where you
work, for years to come.
5. Cutting edge innovations:
With over 65 years of experience
and a line of award winning
products, our design team is on the
Ƥ
hours with our customers to
deliver innovations around your
applications and how you work.
For information on all our Fluke
Special Promotions
ContactEDLElectricalDistributors
Tel: 01 4271444
Email:
sales@edlireland.ie ơ
December 15th 2016